
NewsDetails
What are the precision requirements for drilling tube sheets? How is the hole spacing determined?
author:Kairuifeng time:2026-09-29 22:19:17 Click:109
Question: What are the precision requirements for drilling holes in the tube sheet? How is the hole spacing determined?
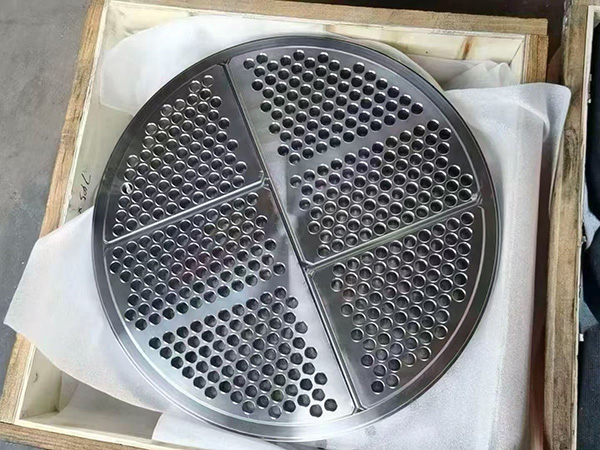
The tube sheet is a core component of shell-and-tube heat exchangers. The drilling accuracy of the tube sheet directly affects the insertion and expansion/welding quality of the heat transfer tubes, as well as the sealing performance and service life of the heat exchanger.
I. Precision Requirements for Tube Sheet Drilling
1. Hole Diameter Accuracy: For expansion joint connections, the tube hole diameter is generally the outer diameter of the heat exchange tube plus 0.2 to 0.4 mm, with a hole diameter tolerance of H12 or H13; for welded connections, it is generally the outer diameter of the heat exchange tube plus 0.5 to 1.0 mm; for combined expansion and welding, it is generally plus 0.3 to 0.6 mm. If the hole diameter is too large, the expansion joint will not be secure; if it is too small, tube insertion will be difficult.
2. Hole Position Accuracy (Hole Spacing Deviation): Generally, the hole position deviation shall not exceed ±0.5 mm; for high-precision requirements, it shall not exceed ±0.3 mm; the deviation of the spacing between adjacent holes shall not exceed ±0.3 mm; and the diagonal deviation shall not exceed ±0.5 mm. Excessive hole position deviation will make it difficult to install the heat exchange tubes.
3. Hole Wall Surface Roughness: For expansion joints, Ra shall not exceed 12.5 micrometers, and there shall be no longitudinal scratches, cracks, or burrs; for welded joints, Ra shall not exceed 25 micrometers. Longitudinal scratches will cause the expansion joint seal to fail.
4. Hole Perpendicularity: The deviation of the hole axis from the perpendicular to the tube sheet surface generally does not exceed 1 degree.
5. Hole Chamfering: Both ends of the pipe holes should be chamfered at 1×45° or 1.5×45°, and deburred to facilitate pipe threading and welding.
6. Flatness of the tube sheet: The flatness of the sealing surface generally does not exceed 0.05 mm.
II. Method for Determining Hole Spacing (Tube Center-to-Center Distance)
1. Determination Principles: Ensure the strength of the tube sheet; insufficient bridge width may lead to tube sheet deformation or cracking; ensure sufficient space for expansion/welding; ensure reasonable fluid flow in the shell side; for economic reasons, the tube pitch should not be too large to avoid increasing the tube sheet size.
2. Common tube pitch values: 19 mm diameter tubes use a 25 mm pitch (bridge width 6 mm); 25 mm diameter tubes use 32 mm (bridge width 7 mm); 32 mm diameter tubes use 40 mm (bridge width 8 mm); 38 mm diameter tubes use 48 mm (bridge width 10 mm); 45 mm diameter tubes use 57 mm (bridge width 12 mm); 57 mm diameter tubes use 72 mm (bridge width 15 mm). The tube pitch is generally 1.25 to 1.4 times the outer diameter of the heat transfer tube, with 1.25 times being the most common.
3. Tube Hole Arrangement: Equilateral triangular arrangement offers high tube sheet utilization, good shell-side fluid turbulence, and high heat transfer efficiency, making it the most commonly used; square arrangement facilitates mechanical cleaning of the shell side and is suitable for applications where the shell-side medium is prone to fouling.
4. Verification of Tube Pitch Calculation: The bridge width is equal to the tube pitch minus the tube hole diameter. Generally, the bridge width is required to be no less than 0.25 times the outer diameter of the heat exchange tube and no less than 6 mm. For example, for a tube with a diameter of 25 mm, a tube hole diameter of 25.5 mm, and a tube pitch of 32 mm, the bridge width is 32 minus 25.5, which equals 6.5 mm, meeting the requirement.
5. Tube Layout Limiting Circle: The distance from the center of the outermost tube hole to the inner wall of the shell is generally not less than 0.25 times the outer diameter of the heat exchange tube.
III. Drilling Machining Process Requirements
1. Drilling Equipment: Radial drilling machine (small batches, large hole diameters), CNC drilling machine (large batches, high precision), multi-axis drilling machine (high efficiency), planar drilling machine (specifically for large tube sheets).
2. Drilling Sequence: Scribing/spotting, trial drilling of the reference hole, drilling, reaming/reaming, chamfering, inspection.
3. Precautions: Ensure the tube sheet is securely fixed; keep the drill bit sharp and replace it promptly; provide adequate cooling and lubrication to prevent burning of the hole walls; regularly inspect hole position accuracy; use dedicated drill bits and cutting parameters for stainless steel tube sheets to prevent work hardening.
IV. Quality Inspection Requirements
1. Hole diameter inspection: Inspect each hole using a plug gauge or vernier caliper, with a sampling rate of no less than 10%;
2. Hole position inspection: Use a dedicated hole spacing template or a coordinate measuring machine (CMM), with a sampling rate of no less than 5%;
3. Surface quality inspection: Visual or magnified inspection of hole wall defects;
4. Verticality inspection: square or dedicated inspection tool;
5. Flatness inspection: surface plate and feeler gauge;
6. Non-destructive testing: ultrasonic testing of the base layer of the tube sheet, and penetrant testing of the overlay layer.
Cangzhou Kairuifeng Pipeline Equipment Co., Ltd. specializes in the production of various heat exchanger tube sheets. Utilizing CNC drilling machines, we ensure high hole position accuracy and support customization for large diameters. We welcome your inquiries and purchases.
 Contact us
—— Contact:Manager
—— Tel:+86 15720204999
—— Email:zeleiliu97@gmail.com
—— Url:https://www.krfpipe.com
—— Address:No. 108 Longhai West Road, Yanshan Town, Yanshan County